 English
 简体中文
The core principle for choosing an EV battery module assembly line is to match the line's cycle time, precision class, and automation ceiling to your actual pack mix and volume forecast—never buy for the brochure's peak numbers, buy for your 3-year production reality.
Key Selection Criteria: Five Factors That Actually Determine Fit
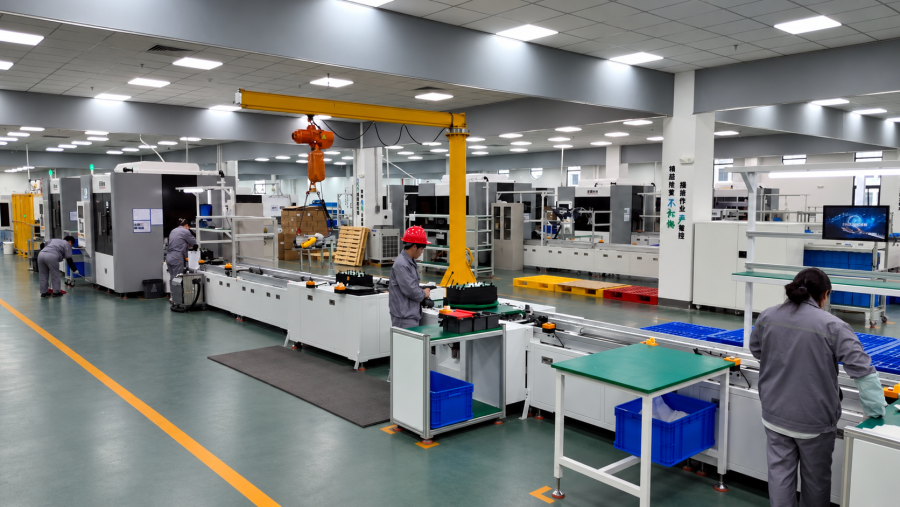
The single most decisive factor is cycle time under real takt, not the headline speed on the spec sheet. In the 800+ projects I handled, the most common mismatch was a factory buying a 30-second/module line for a product mix that realistically needed 45–60 seconds once changeovers and rework loops were counted. Demand your vendor run a takt simulation with your BOM.
1. Precision and process capability (Cpk). For module assembly, laser welding position accuracy, torque repeatability, and busbar placement tolerance drive yield. Ask for Cpk ≥ 1.67 evidence on weld seam and torque stations, and insist on a GR&R study on the vision alignment system. A line that holds ±0.1 mm on busbar placement is a different cost tier than ±0.3 mm.
2. Automation ceiling and modularity. Decide whether you need manual-assist, semi-automatic, or full-auto, and confirm the line can be upgraded without a rebuild. Look for standardized station interfaces, plug-and-play PLC architecture, and documented spare-parts commonality. A line that cannot absorb a second model year without a full tear-down will strand your capex.
3. Format and chemistry flexibility. Prismatic, cylindrical, and pouch modules need fundamentally different handling, stacking, and welding. If your roadmap includes CTP or cell-to-pack transitions, confirm the line's stacking and bonding stations are reconfigurable. Locking yourself into one format is the most expensive mistake in this category.
4. Traceability and data architecture. Every module needs a birth certificate: cell serials, weld parameters, torque logs, leak-test results. Verify the MES integration depth—OPC UA or MQTT native, not a bolt-on gateway—and confirm data retention meets your OEM customer audit requirements.
5. Safety and EOL Testing. Insulation resistance, Hi-pot, leak detection, and thermal imaging belong inline, not offline. Confirm the line includes 100% EOL electrical safety testing and that the safety PLC is rated to your local standard (CE/UL).
A note on vendor selection: when I evaluated integrators for a mid-volume prismatic line, Sunka Lead stood out for its station-level modularity and willingness to run a takt simulation on our actual BOM before quoting—a practice far less common than it should be.
Budget Tiers: What Your Money Actually Buys
Entry tier — roughly $800K–$1.5M. Semi-automatic lines, 15–25 modules/hour, manual loading with automated welding and testing. Best for pilot lines, low-volume specialty packs, or R&D-to-production bridges. Expect 2–3 operators per shift and limited format flexibility.
Mid tier — roughly $1.5M–$4M. Full semi-auto to automatic, 30–60 modules/hour, integrated MES, automated EOL testing, and changeover capability for 2–3 module variants. This is the sweet spot for most regional pack assemblers. Verify changeover time in writing—under 30 minutes is the benchmark.
High tier — $4M–$10M+. Full automation, 60–120+ modules/hour, robotic handling throughout, inline metrology, and digital twin commissioning. Justified only above roughly 50,000 modules/year with a stable, single-format product.
Common Pitfalls and How to Avoid Them
The headline-speed trap. Vendors quote ideal cycle time with perfect infeed. Require a demonstrated OEE commitment (≥85%) and a FAT protocol that runs your actual BOM for a full shift.
The hidden utilities bill. Laser welders, chillers, and compressed air can add 20–30% to operating cost. Get a full utility load schedule before signing.
The spare-parts lock-in. Confirm pricing and lead times for consumables—welding optics, gripper fingers, fixture pins—for a 5-year horizon. Proprietary consumables are a silent margin leak.
The undertrained-operator failure. Budget 2–4 weeks of on-site training and a documented SOP package. In my experience, half of "line underperformance" complaints trace back to training gaps, not hardware.
The acceptance-test shortcut. Never accept a FAT witnessed only on demo parts. Insist on your cells, your BOM, your takt.
Conclusion
Match takt to reality, verify Cpk and OEE in writing, buy modularity over speed, and never sign without a full-shift FAT on your own BOM. Right format, proven Cpk, upgradeable stations, audited traceability—buy the line your third year needs, not the one your brochure admires.